
Cross-linked shrink film is often the stronger starting candidate for demanding packs, but it is not automatically the better film. Non-cross-linked film may be fully adequate for routine products, stable lines, or distortion-sensitive packages. The useful comparison is therefore not the label alone. Buyers should compare an exact grade and gauge by mechanical performance, seal behavior, shrink response, optics, operating window, and total cost per accepted package—then confirm the result on the intended product and equipment.
What Cross-Linking Means in Polyolefin Shrink Film
For regulatory context, consult the U.S. FDA’s food-packaging guidance before approving an intended food-contact use.
In this article, both choices are polyolefin shrink film families intended for comparable packaging work. Cross-linking describes an additional polymer-network change. It does not identify every resin layer, additive, orientation condition, surface treatment, or performance value in the finished film. Those variables remain part of the grade specification.
How irradiation can create links between polymer chains
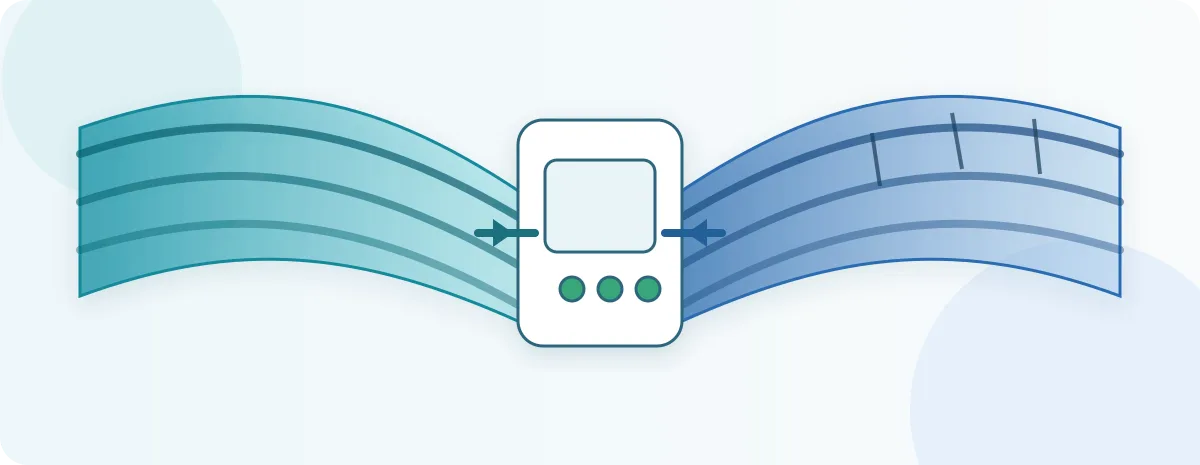
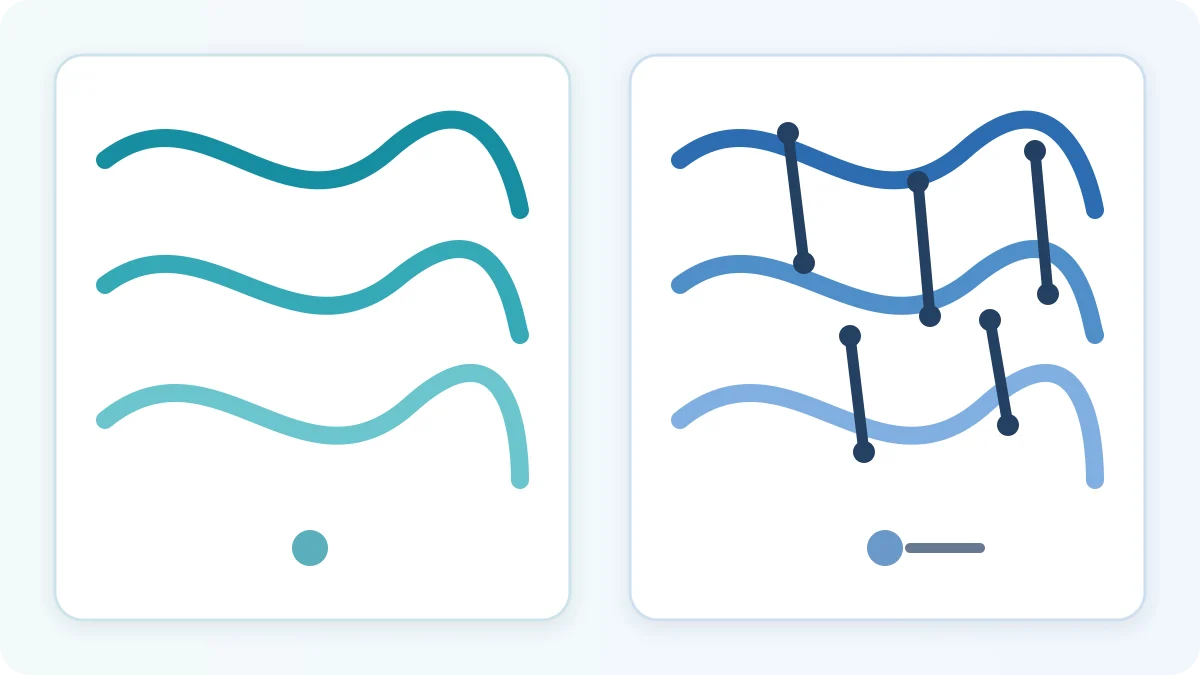
Industrial film producers can expose a polymer structure to ionizing radiation, such as an electron beam. The energy creates reactive sites in the polymer. Some sites form bonds between neighboring chains, producing an inter-chain network. The International Atomic Energy Agency describes this as a three-dimensional network created by direct bonding between polymer chains.
That network can change how.
What non-cross-linked means—and what it does not tell you
Non-cross-linked generally means the film has not received the intentional cross-linking step used for the comparison grade. It does not mean the film is a single-layer material, weak, slow, cloudy, or low quality. A standard film can still use multiple layers, selected resins, controlled orientation, slip systems, and sealant design.
The negative definition also says little about gauge, shrink force, free shrink, seal initiation, impact resistance, or optics. Those values must come from the named grade, measured with stated methods and conditions. Ask suppliers to describe the construction at a commercially appropriate level and to return grade-specific data. If two offers differ in resin family, layer structure, gauge, or intended application, the comparison is not a clean test of cross-linking alone.
Cross-Linked vs. Non-Cross-Linked Shrink Film at a Glance
The table shows useful selection tendencies, not guaranteed category rules. A high-performance standard grade can outperform an unsuitable cross-linked grade on a particular line. Use each row to decide what supplier evidence or trial measurement is needed.
| Comparison axis | Cross-linked film: useful starting hypothesis | Non-cross-linked film: useful starting hypothesis | What to verify |
|---|---|---|---|
| Abuse tolerance | Often shortlisted for sharp edges, heavy packs, repeated punctures, or rough handling | Often suitable where product geometry and distribution abuse are modest | Exact gauge, puncture or impact method, and package trial failures |
| Seal operating window | Selected grades may tolerate variable or demanding sealing conditions | Selected standard grades may still run fast with short dwell and strong seals | Seal temperature, pressure, dwell, cooling, force, and failure mode |
| Shrink behavior | May support demanding shapes or wider processing latitude in a named grade | May be sufficient for stable packages; special grades can offer low shrink force | Free shrink, restrained force, distortion, temperature, and time |
| Optics | High clarity and gloss are available in named grades | High clarity and gloss are also available in named grades | Same gauge, haze method, gloss geometry, and surface condition |
| Downgauging | Toughness may create a trial opportunity at lower gauge | Lightweight standard grades can also be economical | Accepted output, protection, roll yield, rejects, and damage |
| Line fit | A strong candidate for high-risk or variable operations | A strong candidate for proven, stable applications | Actual sealer, tunnel, speed, airflow, perforation, and maintenance state |
The practical difference is the level and type of capability available in a specific formulation. Neither category eliminates the need to compare like with like. Supplier tables should use the same units, test methods, material directions, gauge basis, and conditioning wherever possible.
Strength, Puncture Resistance, and Seal Integrity
“Stronger” is too broad for film approval. Stretching a specimen, propagating a tear, initiating impact damage, and pulling apart a seal are different events. Each needs an appropriate test and a package-level interpretation.
Film-body toughness: puncture, tear, and impact
ASTM D882 addresses tensile properties of thin plastic sheeting. Results depend on specimen thickness, preparation, test speed, grip separation, and direction. ASTM D1922 measures propagation tear resistance, not the force needed to create the initial cut and not total package toughness. MD and TD results should remain separate.
Impact methods also answer different questions. ASTM D1709 reports the dart mass associated with 50% specimen failure under a defined method. Method A and Method B are not interchangeable. ASTM D4272 measures energy absorbed through impact and failure, so it should not be presented as an equivalent number.
For a fair grade comparison, record actual thickness and test films in the same direction under the same conditions. Then connect laboratory results to the failure observed in use. A sharp carton corner may drive local puncture. A nick near a seal may become a propagation tear. A dropped multi-pack may create impact and seal loads together. No single value predicts all three.
Seal behavior: strength, consistency, and failure mode
A film body can survive handling while its seal fails. Conversely, a high peel force can hide an undesirable failure in the film beside the seal. ASTM F88/F88M measures the force required to separate a flexible-material seal and calls for the failure mode to be recorded. The test technique must remain consistent because specimen support and peel geometry affect the result.
Build a seal study around the actual process. Record seal temperature, dwell time, pressure, jaw condition, cooling, line speed, specimen width, pull speed, conditioning, and failure mode. Sample across the expected operating window, not only at the best setting. Compare average force and variation, then inspect for peel, cohesive failure, tearing next to the seal, burn-through, channels, or contamination.
ASTM provides a method, not a universal acceptance limit. The buyer must set limits from package mass, handling, opening expectations, distribution hazards, and quality risk. The preferred film is the one that repeatedly stays inside that application-specific window.
Shrink Response, Optics, and Packaging-Line Behavior
Shrink percentage, force, appearance, and machine behavior interact. A film that looks excellent in an unrestrained laboratory bath may distort a flexible product or behave differently in a tunnel with uneven airflow. Approve these attributes as a system.
Shrink force, free shrink, and product distortion
Free shrink and shrink force are not synonyms. ASTM D2732 determines the unrestrained linear dimensional change of a plastic film at a specified temperature. It helps describe how much a specimen can contract when it is free to move. ASTM D2838 addresses shrink tension and orientation release stress under restraint.
Record temperature, exposure time, MD and TD direction, specimen preparation, and procedure. Higher free-shrink percentage does not automatically create a better package. The film must pull the web into the desired shape without crushing trays, curling paperboard, bending delicate components, or creating excessive edge stress. Distortion-sensitive products may need a grade with deliberately lower shrink force even when a tougher grade is available.
Clarity, haze, gloss, and gauge effects
Clarity is often used as a broad sales term. A controlled comparison should separate haze, gloss, visible defects, wrinkles, and print presentation. ASTM D1003 covers haze and luminous transmittance for transparent plastics. ASTM D2457 covers specular gloss at defined geometries. A haze result and a gloss result are not interchangeable.
Compare samples at the same actual gauge with the same measurement method and surface orientation. Thinness can affect handling and final appearance even when the resin system is unchanged. Also inspect the finished package under agreed lighting. Laboratory optics cannot fully represent wrinkles, dog-ears, seals, perforation patterns, scuffs, or the visual effect of film tension over printed graphics.
Sealer and tunnel settings, throughput, and residue
Start with the current qualified settings and a maintained machine. Then record changes rather than relying on a generic “more heat” or “less heat” claim.
- Log sealer temperature or power, dwell, pressure, knife or wire condition, cooling, and film tension.
- Log tunnel-zone temperatures, conveyor speed, airflow direction, damper position, and product spacing.
- Count accepted packages, start-up waste, burn-through, weak or open seals, wrinkles, dog-ears, distortion, and rework.
- Record film tracking, static, perforation performance, changeover duration, stoppages, and deposits on sealing components.
- Retain samples from normal operation and from the edges of the acceptable operating window.
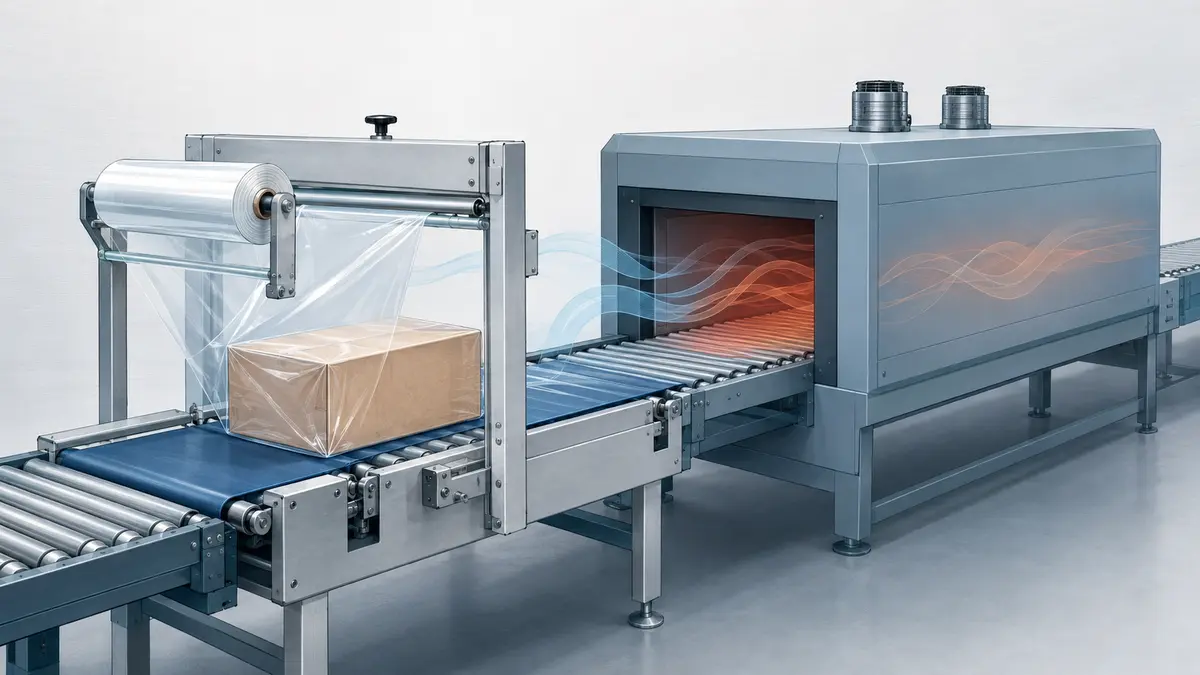
Excess tunnel heat, poor airflow, incorrect perforation, unstable tension, or worn sealing parts can resemble a film problem. Correct obvious equipment faults before declaring either category unsuitable. A wider operating window is valuable only when the target grade demonstrates it on the buyer’s line.
When Cross-Linked Shrink Film Is the Better Starting Point
Cross-linked film deserves priority when the cost or frequency of package failure is high and a supplier offers a grade designed for that risk. It is a shortlist decision, not an approval decision.
High-risk products and high-output lines
Use the following matrix to translate a risk signal into a trial action.
| Observed condition | Why a cross-linked grade may be shortlisted first | Trial evidence required | Important boundary |
|---|---|---|---|
| Sharp corners or irregular contact points | Greater abuse tolerance may reduce local puncture or tear initiation | Failure count by location, retained samples, impact or distribution check | Geometry and gauge still control stress concentration |
| Heavy multipacks | Higher loads can combine film-body and seal stress | Seal failure mode, lift/handling test, distribution simulation | Strong film does not repair an undersized seal |
| Frequent burn-through or variable seals | A named grade may offer a broader demonstrated sealing window | Window map across speed, dwell, temperature, and pressure | Diagnose jaw condition and tension first |
| High-output line with costly stops | Wider processing latitude or a lower validated gauge may improve output | Accepted packages per hour, stops, waste, roll changes | High speed alone does not require cross-linking |
| Current package damage or field failures | Added toughness may address an identified film-body failure | Root-cause evidence and representative transport trial | Film cannot correct every product or machine cause |
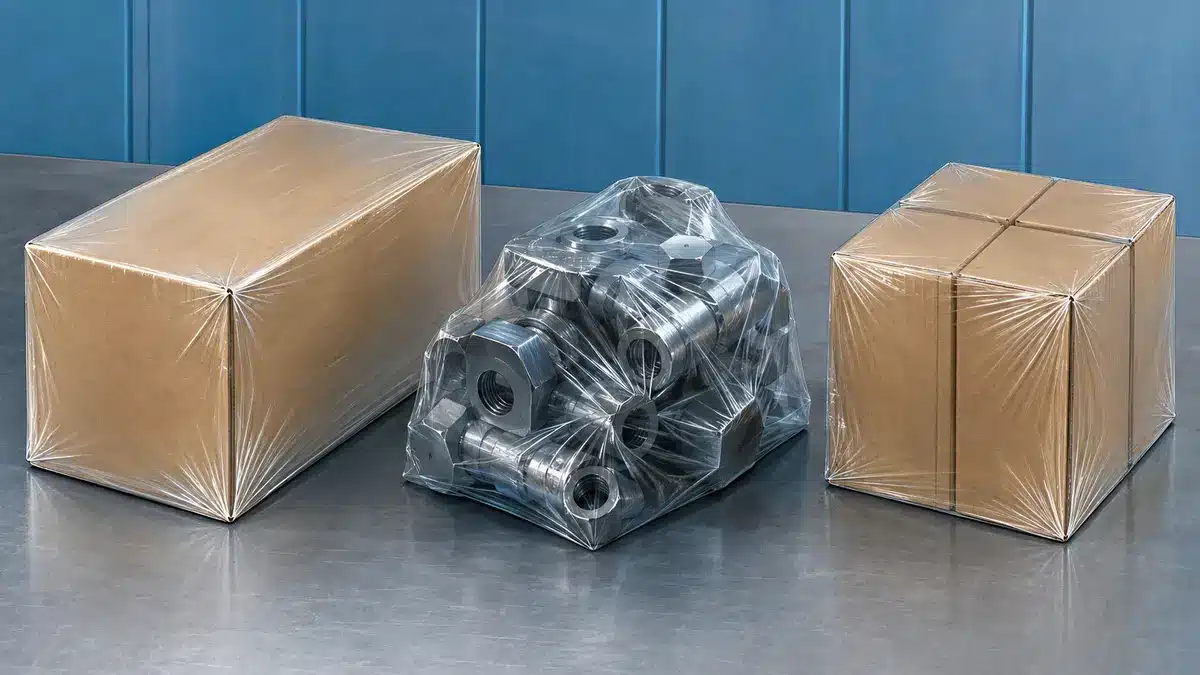
Cross-linked film is also a reasonable first trial when the buyer wants to explore downgauging without surrendering protection. The lower gauge must still meet seal, shrink, appearance, handling, and distribution criteria. Do not treat a supplier’s broad portfolio statement as proof for every cross-linked grade.
When Non-Cross-Linked Shrink Film May Be the Better Fit
Standard film should remain on the shortlist when the application is predictable and the required performance is already achieved. Buying more capability than the package uses can add qualification work without improving accepted output.
Standard products, existing equipment, and cost discipline
A non-cross-linked grade may be the better first trial when products have smooth geometry, modest mass, limited abuse exposure, and stable package dimensions. It may also fit an established line with a documented operating window and low reject rate. Importantly, a standard grade can still be designed for high-speed operation, short sealing dwell, strong seals, and good optics. Those are grade claims to verify, not exclusive properties of either category.
Keep the standard candidate when it passes these checks:
- The current film does not show recurring puncture, impact, tear, or seal failures.
- The sealer and tunnel run consistently at the required output without a narrow or unstable window.
- Appearance, shrink, distortion, and handling limits are met at the proposed gauge.
- Distribution testing and field history show adequate protection.
- The cost per accepted package is competitive after waste, downtime, labor, energy, and damage are counted.
For delicate trays, paper products, or easily distorted components, specify the required low shrink force directly. Do not assume that non-cross-linked automatically means lower force. Approve the named grade on the real product.
Compare Total Packaging Cost, Not Film Price Alone
Roll price is an input, not the economic result. Gauge, roll dimensions, yield, changeovers, scrap, speed, energy, rework, and damage can reverse an apparent price advantage. Compare candidates over the same accounting boundary and representative production period.
A cost-per-accepted-package model
Use this symbolic model:
Cost per accepted package = (film consumed + direct operating labor + changeover cost + downtime cost + scrap and rework + attributable energy + package-related damage or returns) ÷ accepted packages produced
Define every variable before the trial. Film consumed should come from actual roll usage or verified length and width, not nominal package count alone. Changeover cost can include lost production and labor. Downtime needs an agreed costing rule. Energy should be included only when it can be measured or consistently estimated. Damage and returns need a clear causal and time boundary.
The denominator is accepted packages, not total cycles. Rejected packs consumed material and machine time but did not create usable output. Report start-up waste separately so a short demonstration does not hide it.
Thinner gauges can increase area yield. Longer rolls can reduce roll changes. Neither guarantees lower total cost. A thinner film that creates weak seals, distortion, or more field damage may be more expensive. A higher-priced film can be economical if measured uptime or protection gains exceed its premium. Use the buyer’s production data; supplier case studies are hypotheses, not savings forecasts.
How to Validate a Shrink Film Before Approving It
Approval should combine controlled line evidence, method-aware laboratory data, and procurement documentation. Define pass/fail criteria before seeing the result. Otherwise, teams can unconsciously move the goalposts toward the preferred supplier.
Run a controlled machine and package trial
- Freeze the baseline. Record the incumbent grade, lot, actual gauge, roll dimensions, product configuration, machine condition, settings, output, defects, waste, and acceptance criteria.
- Confirm comparability. Match width and intended application. Document construction, nominal gauge, measured thickness, lot, storage, and conditioning for each candidate.
- Change one material variable at a time. Start from a safe supplier-recommended setting, then map the operating window while holding product, operators, package pattern, and inspection rules stable.
- Measure both process and package outcomes. Count accepted output, rejects, interruptions, roll changes, seal failures, burn-through, wrinkles, distortion, optics issues, and film-body damage.
- Challenge the package. Perform the relevant handling, impact, sharp-point, distribution, aging, or environmental checks. Use the same protocol for every candidate.
- Review total cost and risk. Calculate cost per accepted package, examine failure modes, and document any trade-off. Repeat if the run was too short or unrepresentative.
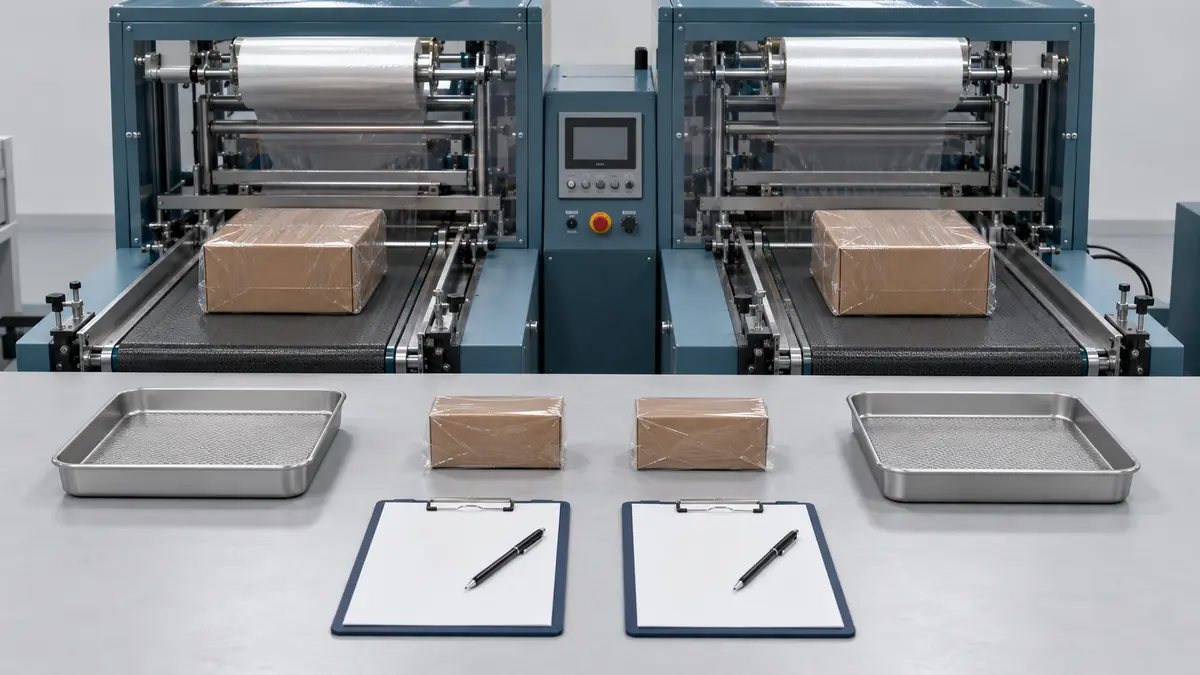
Keep retained samples and raw observations. A single attractive package made at a tuned setting is not enough to establish a robust production window.
Specify tests, conditions, and RFQ evidence
Laboratory reports are comparable only when their basis is visible. ASTM D618 provides conditioning practices for plastics. ASTM D6988 addresses thickness determination for film specimens. These controls matter because gauge and conditioning can shift mechanical results.
Request the following in the RFQ or technical comparison sheet:
- Manufacturer, exact grade, construction description, lot or batch identity, production date, and intended use.
- Nominal gauge and tolerance, measured thickness method, width, length, core, winding direction, maximum roll diameter, and splice policy.
- Test method and edition, specimen direction, conditioning, temperature, humidity, speed, and units for each reported value.
- Tensile, tear, impact or puncture data relevant to the risk; seal method, sealing conditions, force, variability, and failure mode.
- Free-shrink values by MD and TD with time and temperature; restrained shrink-force data when distortion matters.
- Haze and gloss with the stated method and geometry, plus finished-package appearance criteria.
- Clear identification of typical values versus guaranteed specification limits.
- Product- and market-specific compliance documents where required, plus sample-roll and line-trial support.
Standards define test procedures. They do not decide the buyer’s minimum strength, maximum haze, acceptable distortion, or required production rate. Put those limits in the approval plan.
Frequently Asked Questions
Is cross-linked shrink film always stronger than non-cross-linked film?
No. A named cross-linked grade may have higher values in selected tests, but “strength” covers several non-equivalent properties. Compare exact grade, actual gauge, MD or TD direction, conditioning, and method. Tensile, propagation tear, dart impact, total impact, puncture, and seal force answer different questions.
Can cross-linked film always be downgauged?
No. Added toughness can create a useful downgauging opportunity, but the lower gauge must preserve accepted-package output. Verify seals, shrink, appearance, handling, distribution protection, operating window, roll yield, rejects, and total cost. There is no universal safe gauge reduction.
Does cross-linked film require more tunnel heat?
Not necessarily. Heat demand depends on the exact grade, gauge, tunnel design, airflow, conveyor speed, perforation, package geometry, and desired appearance. Use supplier starting guidance, then map the operating window. Do not assign one temperature rule to either category.
Which film is better for sharp or irregular products?
Cross-linked film is often the more sensible first candidate because selected grades target demanding shapes and puncture risk. It is not mandatory. Locate the real stress points, compare suitable gauges, inspect seal placement, and run a representative handling or distribution trial before approval.
Is non-cross-linked shrink film more recyclable?
That cannot be concluded from cross-link status alone. The APR Design Guide evaluates packaging in the context of the complete design and recycling pathway. Construction, attachments, inks, labels, collection, sortation, reprocessing, acceptance, and end markets can all matter. Assess the exact package in its destination market and avoid an unconditional recyclability claim.
What data should suppliers provide for a fair comparison?
Ask for exact grade and lot identity, construction, gauge and dimensions, test methods and editions, MD/TD data, conditioning and test settings, typical values versus specification limits, applicable compliance evidence, and trial support. If the basis of a value is missing, treat it as non-comparable until clarified.
Choose by Verified Fit, Not by the Label Alone
Cross-linked film is a strong starting candidate for demanding geometry, abuse, variable sealing conditions, or a carefully controlled downgauging trial. Non-cross-linked film can be the better fit when a standard grade already meets package, line, appearance, protection, and cost requirements. Neither label is an approval.
Define the failure risks and acceptance limits first. Compare exact grades on the same methods, gauge basis, product, equipment, and accounting boundary. Then approve the film that produces stable seals, acceptable shrink and optics, protected products, reliable throughput, and the lowest defensible cost per accepted package.
 English
 Japanese
 French
 Spanish
 Korean
 Italian
 Portuguese
 Dutch
 Arabic
 Russian
 German